Activated Carbon Solutions
Activated Carbon for Water Purification
Water & Wastewater Purification Using Activated Carbon
Activated carbon plays a vital role in modern water purification systems due to its exceptional adsorption capabilities. Produced from organic materials like coconut shells, coal, or wood, it undergoes a special activation process that creates a highly porous structure. This large surface area allows it to capture and hold a wide range of contaminants, improving water clarity, taste, and overall quality.
How Activated Carbon Works
Activated carbon removes impurities through adsorption, a process where unwanted chemicals and particles attach to its porous surface. This makes it highly effective for both small-scale and large-scale water treatment systems.
Key Applications in Water & Wastewater Treatment
- Drinking Water Treatment
- Chlorine & Chloramine Removal.
- Taste & Odor Improvement
- Pesticides & VOC Reduction
- Industrial Wastewater Treatment
- Chemical Contaminant Removal
- Heavy Metal Assistance
- Municipal Wastewater Treatment
- Reduces nitrogen
- Toxic Substance Removal
- Aquariums & Aquaculture Systems
- Enhanced Water Clarity
- Healthier Ecosystems
Activated Carbon for Air Purification
How Activated Carbon Works
1. Adsorption Process
Activated carbon traps gas molecules on its porous surface, effectively removing impurities from the air.
2. Chemical Reactions
Chemically treated or impregnated activated carbon can neutralize specific gases such as ammonia, acid gases, and sulfur compounds, making it suitable for targeted applications.
Applications of Activated Carbon in Air Purification
- Odor Control
- Removal of VOCs
- Toxic Gas Control
- Industrial Emission Treatment
- Indoor Air Quality Enhancement
- Smoke & Fume Control
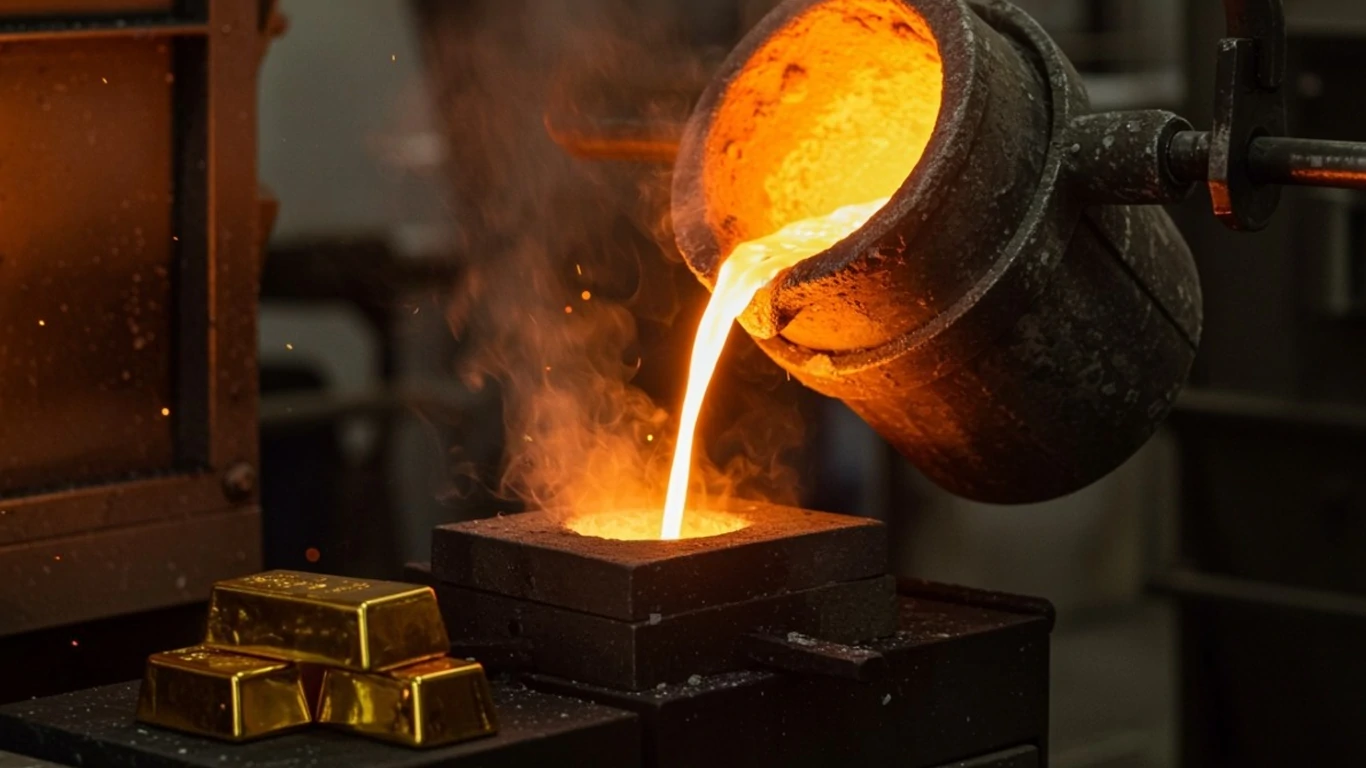
Activated Carbon for Gold Recovery
Activated carbon is an essential material in gold extraction due to its exceptional adsorption capacity and strong affinity for gold cyanide complexes. It is the backbone of the most widely used gold recovery methods – Carbon-in-Pulp (CIP), Carbon-in-Leach (CIL), and Carbon-in-Column (CIC). These processes make gold extraction more efficient, scalable, and cost-effective for mining operations of all sizes.
How Activated Carbon Works in Gold Recovery
- Adsorption of Gold Cyanide Complexes
- High Surface Area & Porosity
- Selective Adsorption
Advantages of Using Activated Carbon
- High Recovery Efficiency
- Cost-Effective
- Flexible & Scalable
- Environmentally Friendly
Steps in the Gold Recovery Process
- Gold Leaching
- Carbon Adsorption (CIP/CIL)
- Carbon Separation
- Elution
- Electrowinning
- Carbon Regeneration
Activated Carbon in Sugar Refining
Activated carbon is an essential component in modern sugar refining. Its ability to adsorb colored compounds, organic impurities, and off-flavors ensures high-quality, food-grade sugar. Used in both cane and beet sugar processes, it helps produce brighter, purer, and tastier sugar for industrial and consumer applications.
How Activated Carbon Works in Sugar Refining
- Decolorization
- Removal of Organic Impurities
- Odor and Taste Adsorption
- Polishing Filter
Applications
- Cane Sugar Refining – Removes residual colorants and impurities after preliminary clarification.
- Beet Sugar Refining – Reduces color and taste-altering organic compounds.
- High-Quality Sugar Production – Used for pharmaceutical- or food-grade sugar.
- Liquid Sugar Refining – Purifies sugar syrups for beverages, confectionery, and industrial use.
Process of Using Activated Carbon
- Preparation
- Carbon Addition
- Adsorption
- Filtration
- Further Refining
Types of Activated Carbon
- Powdered Activated Carbon (PAC)
- Granular Activated Carbon (GAC)
Activated Carbon Delays Ripening in Fruits and Vegetables
Activated carbon is an effective solution to slow the ripening process of fruits and vegetables. By adsorbing ethylene – the natural plant hormone responsible for ripening – and other volatile organic compounds, activated carbon helps maintain freshness, flavor, and texture while extending shelf life during storage and transport.
How Activated Carbon Works
- Ethylene Adsorption
- Absorption of Other Gases
- Maintaining Optimal Storage Conditions
Applications in Food Storage
- Packaging
- Cold Storage Facilities
- Modified Atmosphere Packaging (MAP)
- Fruit Ripening Rooms
Example Applications
- Bananas – Delays ripening during storage and transport.
- Tomatoes – Maintains freshness by controlling ethylene exposure.
- Apples – Preserves crispness and flavor.
- Avocados – Slows natural ripening under controlled conditions.
Types of Activated Carbon for Ripening Delay
- Granular Activated Carbon (GAC)
- Powdered Activated Carbon (PAC)
- Impregnated Activated Carbon
Activated carbon is a versatile, safe, and efficient solution for maintaining the quality and shelf life of fresh produce, helping reduce waste and increase profitability.
Activated Carbon in Wine Decolorization
Activated carbon is an essential tool in modern winemaking for decolorization and correction of certain wine faults. Its porous structure and high surface area allow it to selectively adsorb pigments, phenolic compounds, and other molecules responsible for off-flavors or undesirable color, without significantly affecting the wine’s quality.
How Activated Carbon Works
Activated carbon removes unwanted compounds through adsorption, trapping color-causing pigments, sulfur compounds, and other organic molecules. This process helps correct over-extraction, oxidation browning, or smoke-tainted wines while maintaining the desirable aromas and flavors.
Applications in Winemaking
- Decolorization
- Removal of Off-Flavors and Odors
- Correction of Wine Faults
Types of Activated Carbon for Wine Decolorization
- Powdered Activated Carbon (PAC)
- Granular Activated Carbon (GAC)
Key Considerations for Winemakers
- Conduct bench trials to determine impact on flavor and aroma.
- Use food-grade, enology-specific activated carbon.
- Monitor the wine closely to avoid over-adsorption of desirable compounds.
Activated carbon is a versatile and reliable tool for winemakers, helping fine-tune color, flavor, and overall quality.
Activated Carbon for Energy Storage (Supercapacitors)
Energy storage technology is rapidly advancing, and supercapacitors are becoming essential for reliable, high-power applications. Clean, efficient, and long-lasting, supercapacitors are now widely used in consumer electronics, renewable energy systems, electric vehicles, transportation, lifts, aircraft, and many other sectors.
Powerful yet environmentally friendly, they offer quick charge–discharge cycles and long operational life, making them a critical component in the future of energy solutions.
Carbon Dynamics Australia develops and manufactures activated carbons specifically optimized for supercapacitors. Each carbon grade is engineered to meet and exceed performance needs—whether you require higher energy density, increased power output, or specialized carbon tailored to your electrolyte system. Our solutions ensure consistent performance, durability, and efficiency across all supercapacitor applications.
Wood Based Powdered Activated Carbon
Our wood-based powdered activated carbon is engineered with a well-developed pore structure and high specific surface area, delivering excellent adsorption capacity and rapid filtration performance. With low ash content and a balanced mesopore distribution, it is ideal for liquid-phase decolorization and purification applications.
This grade offers reliable and efficient removal of impurities, pigments, and organic compounds, ensuring clarity, purity, and improved product quality across multiple industries.
Applications
- Food & Beverage
- Fruit Juice
- Wine & Spirits
- Bottling & Brewing
- Edible Oil Refining
- Pharmaceutical Processing
- Environmental Water Treatment
Reagglomerated Acid-Washed Activated Carbon
Reagglomerated acid-washed activated carbon is designed for high-efficiency purification of liquids and water. Its low acid-soluble iron content, high abrasion resistance, and large pore volume ensure rapid adsorption. Reagglomeration creates optimal transport pores, enhancing adsorption speed and overall performance.
Types
- HQ-R-AW: Suited for ultra-pure water, home water filters, and process water applications.
- HQ-D-AW: High molasses number with excellent decolorization capabilities; ideal for purifying acids, sweeteners, syrups, lactic acid, high fructose, and other liquid chemicals.
Applications
- Food & Beverage
- Lactic Acid
- High-Purity Phosphoric Acid
- High-Purity Hydrochloric Acid
- Various Organic & Inorganic Acids
- Sweeteners / Corn Sweetener
- Liquid Chemicals
- Hemodialysis
- Ultra-Pure Water
- Fructose & Glucose
- Drinking Water (Potable) & Decaffeination
- Industrial Processes
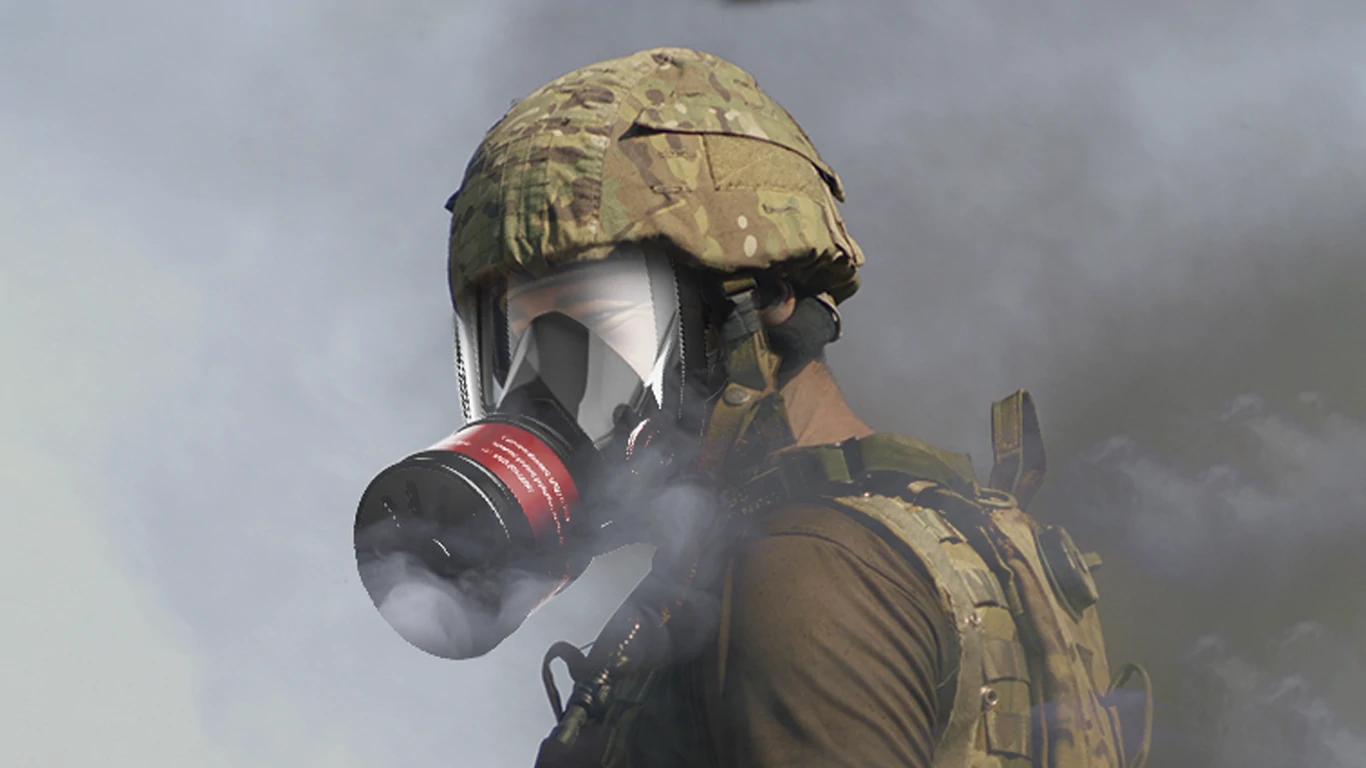
Activated Carbon for Gas Masks
Activated carbon is a critical component in gas masks, offering high adsorption efficiency for harmful gases, vapors, and odors. Its porous structure, combined with chemical impregnation, allows it to neutralize toxic substances, ensuring breathable air for users in military, industrial, and emergency scenarios.
How Activated Carbon Works
- Adsorption
- Impregnation for Specific Gases
Applications
- Military Gas Masks
- Industrial Masks
- Emergency & First Responder Masks
- Personal Protective Equipment (PPE)
- Environmental Hazards
Key Properties for Gas Masks
- High adsorption capacity for a wide range of gases and vapors
- Impregnated carbon for specific toxic gas neutralization
- Thermal stability for high-temperature environments
- Mechanical durability to prevent dust and particle release
- Low airflow resistance for comfortable breathing
Impregnated Carbon for Specific Gases
- Acid Gases (SO₂, HCl): Treated with alkaline compounds like sodium hydroxide.
- Ammonia (NH₃): Treated with phosphoric or other acidic agents.
- Mercury Vapor: Impregnated with sulfur compounds.
- Organic Vapors & VOCs: Adsorbed using high-grade activated carbon.
- Chlorine Gas (Cl₂): Neutralized with reactive impregnated compounds.
Gas Mask Design Features
- Filter Cartridge:
- Multi-Layer Structure:
- Breathability:
- Compatibility: